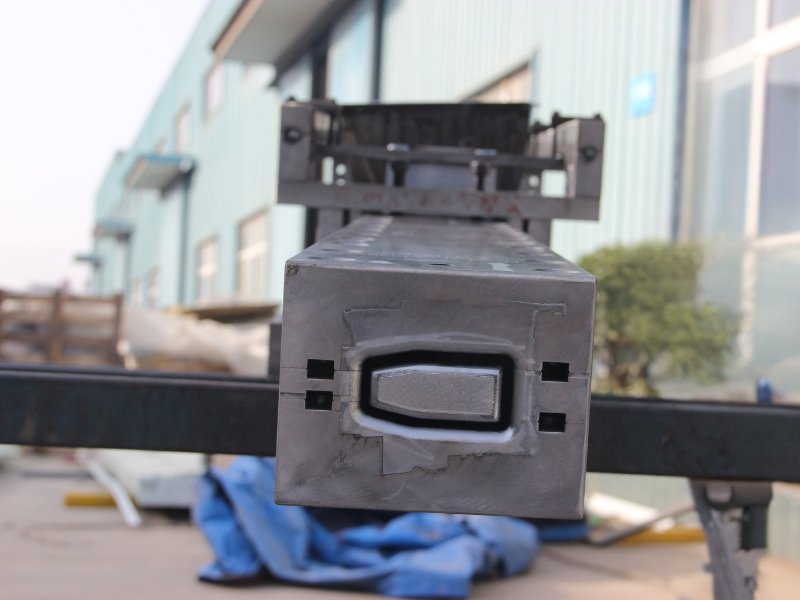


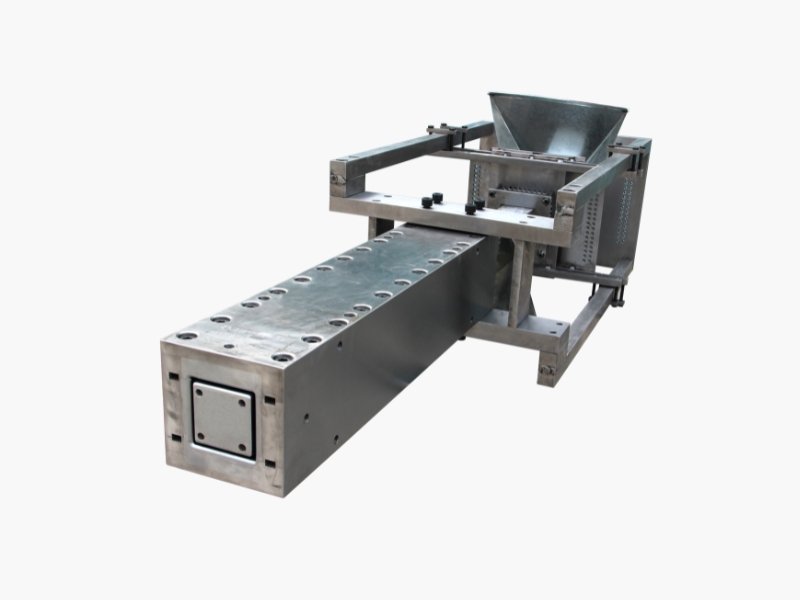
Custom FRP Tube Pultrusion Die for Pultrusion Machine
This high-precision FRP Tube Pultrusion Mold delivers stable dimension, low wear, and long service life, ideal for industrial GFRP pultruded tube mass production.| Parameter Item | Core Specification |
| Mold Material | H13 hot work tool steel, fully heat treated |
| Surface Hardness | HRC 58-62, high wear resistance |
| Cavity Tolerance | ±0.02mm, ensures consistent FRP tube dimension |
| Standard Tube Size Range | Round φ10-76mm, Square 10-100mm |
| Heating System | Integrated cartridge heaters with K-type thermocouples |
| Surface Treatment | Polished to Ra ≤ 0.8μm, smooth demolding |
| Custom Service | Supports non-standard FRP tube profile customization |
Contact Our Team
Get professional support for pultrusion equipment, dies, and profilesDetailed Introduction to FRP Tube Molds
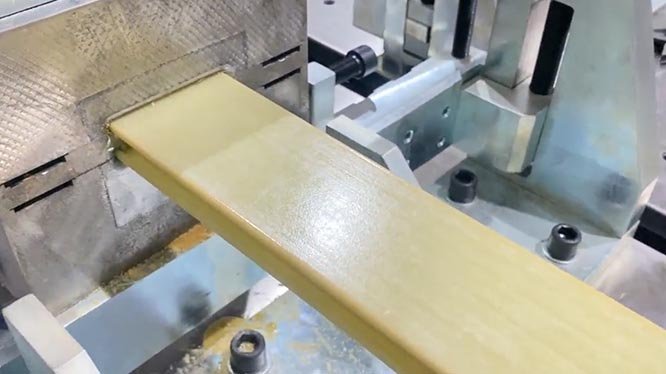
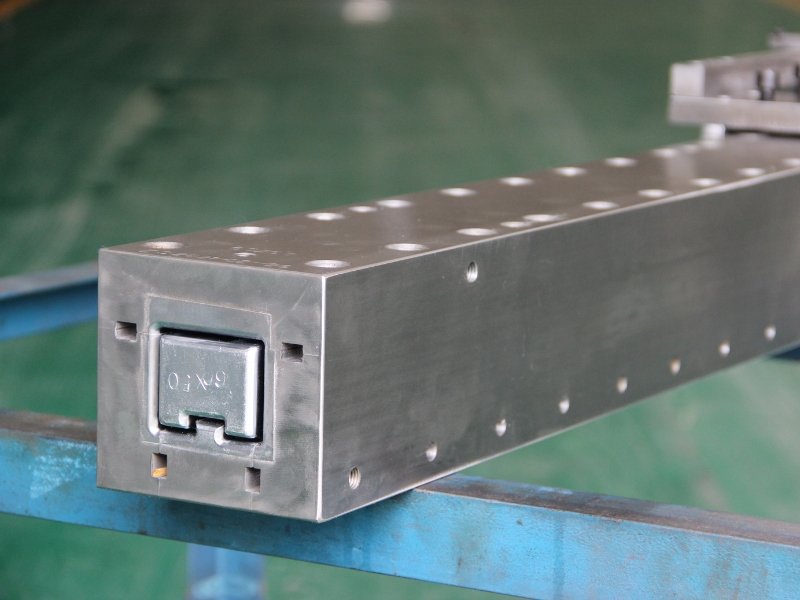
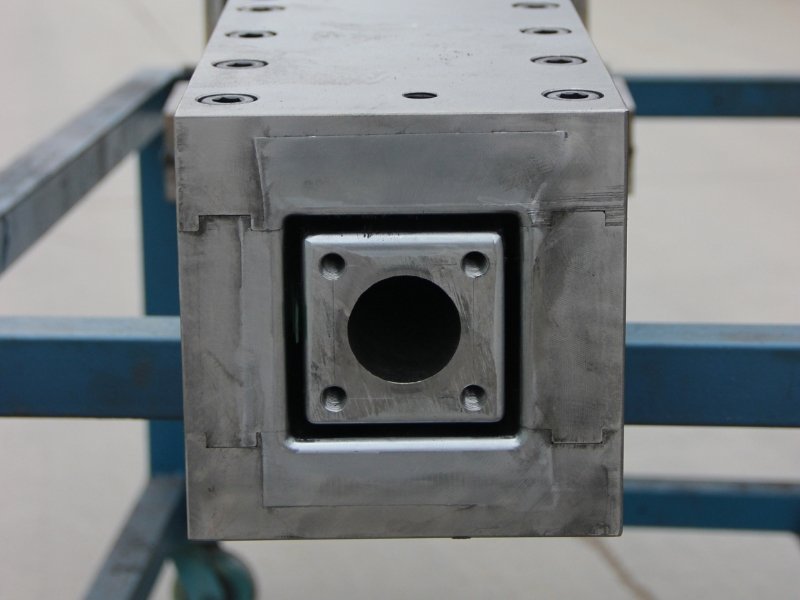
TOLIKE FRP Tube Pultrusion Mold is engineered for continuous pultrusion lines, delivering steady forming accuracy for both round and square fiberglass hollow profiles. Unlike common generic dies, this mold adopts a one-piece precision cavity structure, which effectively eliminates profile warping, surface burrs and dimension deviation during long-time high-speed pulling. It works seamlessly with our matched FRP Pultruded Square Tube and FRP Pultruded Round Tube production processes, helping fabricators maintain consistent product quality across every production batch. This high-performance GFRP tube pultrusion die is manufactured from heat-treated hot work tool steel, with the inner cavity polished to ultra-low roughness. Its optimized heating zone layout ensures uniform resin curing across the entire profile section, drastically reducing mold cleaning frequency and lowering unplanned downtime. For industrial buyers, this directly translates to higher line output, less material waste and lower long-term operating cost compared with standard pultrusion tooling. For custom profile projects, TOLIKE FRP pultrusion tube mold can be adjusted according to special section requirements, supporting non-standard fiberglass pipe dimensions and wall thickness customization. It is a reliable long-life tooling choice for manufacturers who need to stably supply structural, insulating or corrosion-resistant FRP tubular products to downstream construction, energy and infrastructure markets.
Advantages of Our FRP Tube Pultrusion Die

Parameters for GFRP Tube Pultrusion Mold
|
Parameter |
Specification |
Buyer Value |
|
Mold Material |
H13 hot work tool steel, vacuum heat treated |
High-temperature stability, safe for long continuous pultrusion |
|
Cavity Hardness |
HRC 58-62 |
Withstands glass fiber abrasion, extends tooling life |
|
Cavity Tolerance |
±0.02mm |
Consistent FRP tube dimension, fewer rejects |
|
Inner Surface Roughness |
Ra ≤ 0.8μm, mirror polished |
Smooth demolding, defect-free profile surface |
|
Standard Round Tube Range |
φ10-76mm |
Covers most common FRP round tube sizes |
|
Standard Square Tube Range |
10×10-100×100mm |
Ready for mainstream square profile orders |
|
Heating System |
Multi-zone cartridge heaters with K-type thermocouples |
Uniform resin curing, stable production line speed |
|
Working Temperature |
Up to 200℃, adjustable |
Compatible with common polyester and vinyl ester resins |
|
Production Line Speed |
Matched up to 0.3-1.2 m/min |
Supports medium to high output pultrusion lines |
|
Service Life |
1,000,000+ m pulling (typical) |
Lower cost per meter, better long-term ROI |
|
Customization |
Non-standard section, wall thickness and length |
Fits special project and OEM requirements |
|
Delivery & Support |
Pre-tested before shipment, mold trial plus technical guidance |
Shorter commissioning and new product launch cycle |

Manufacturing Process of FRP Tube Pultrusion Die
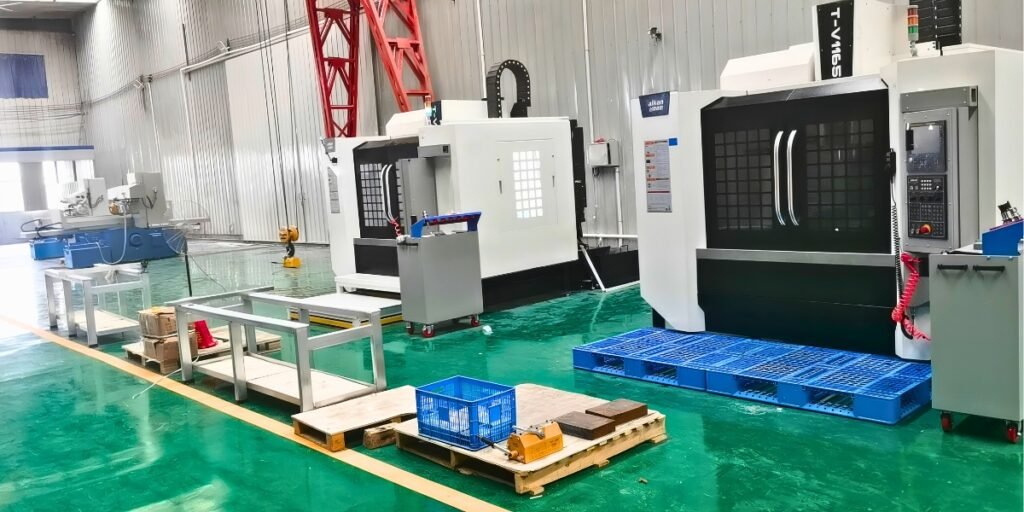
Manufacturing Process of FRP Tube Pultrusion Mold starts with strict material selection and precision CNC machining, which defines the final forming accuracy and long service life of the FRP pultrusion tube die. Every TOLIKE FRP tube pultrusion mold is based on high-quality hot work tool steel blank, and all raw materials will go through incoming inspection to ensure no internal crack or impurity before formal processing. This step lays a solid foundation for the high wear resistance and high temperature stability required by long-term continuous pultrusion production.
After blank preparation, the core cavity of the fiberglass tube pultrusion mold is processed through multi-axis CNC milling and high-precision grinding. For round and square FRP tubular profiles, the inner cavity geometric accuracy is strictly controlled within ±0.02mm, and the flow channel transition is optimized to avoid resin retention and uneven curing during pultrusion. This process also ensures the inner wall of the GFRP pipe pultrusion die obtains a uniform and smooth base, which is a key prerequisite for subsequent polishing and easy demolding performance.
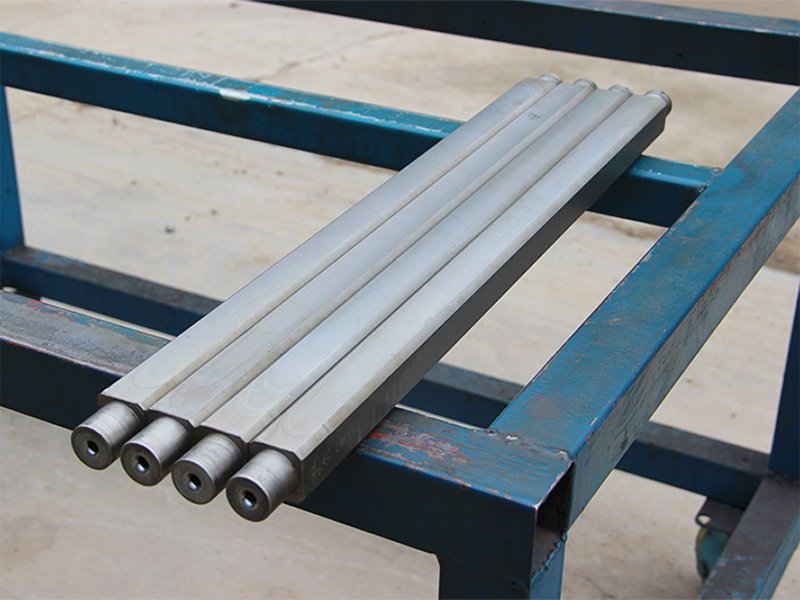
Then the FRP pultrusion die enters vacuum heat treatment and fine surface treatment. After high-temperature quenching and tempering, the overall hardness of the mold cavity reaches HRC 58-62, which greatly improves the ability to resist continuous friction from glass fiber roving and resin. The inner cavity is then manually polished step by step to mirror effect, making the surface roughness lower than Ra 0.8μm, effectively reducing profile surface burrs, fiber fuzzing and demolding resistance in mass production.
Then the FRP pultrusion die enters vacuum heat treatment and fine surface treatment. After high-temperature quenching and tempering, the overall hardness of the mold cavity reaches HRC 58-62, which greatly improves the ability to resist continuous friction from glass fiber roving and resin. The inner cavity is then manually polished step by step to mirror effect, making the surface roughness lower than Ra 0.8μm, effectively reducing profile surface burrs, fiber fuzzing and demolding resistance in mass production.
Manufacturing Process for Pultrusion Dies:
Available Section Shapes and Corresponding Profile Applications
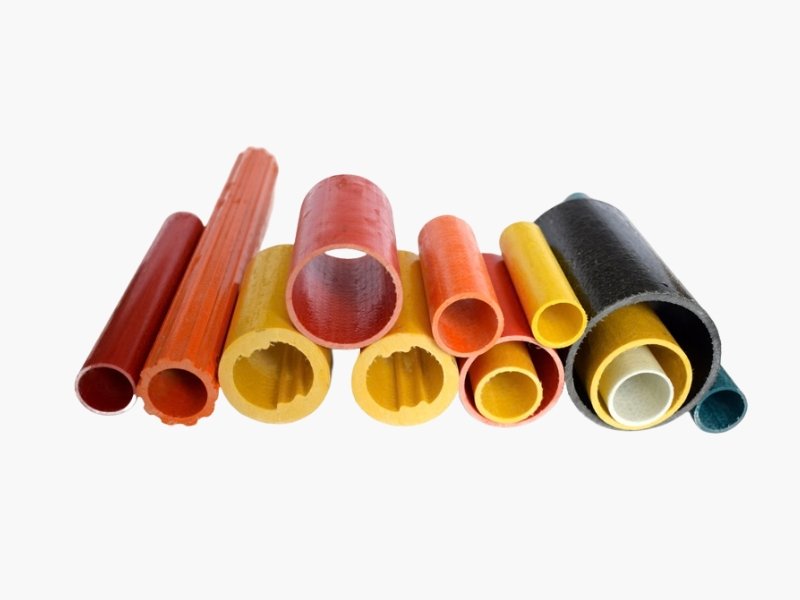
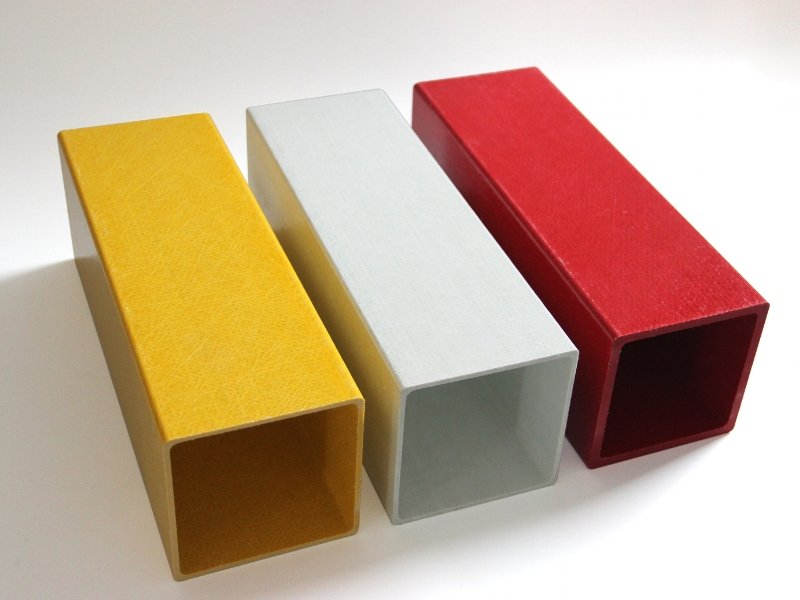
TOLIKE FRP Tube Pultrusion Die supports a wide range of customizable hollow section profiles, covering almost all mainstream FRP tubular shapes required by industrial pultrusion lines. The most standard configurations include solid round tube, hollow round tube, square tube and rectangular tube, which are the most in-demand fiberglass profiles for general structural and insulating applications. Beyond these basic shapes, the FRP pultrusion tube mold can also be designed for special sections such as elliptical tube, D-shaped tube, multi-lumen hollow tube and grooved inner wall tube, to meet non-standard engineering requirements that ordinary profile tooling cannot cover.
These different shapes of FRP profiles produced by the fiberglass tube pultrusion die have formed highly targeted application scenarios in multiple downstream industries. Round FRP pultruded tubes are widely used for electric power insulation rods, telecom antenna support poles, fence posts and cable protection ducts, leveraging their uniform circumferential strength and excellent bending resistance. Square and rectangular FRP tubes are more favored in construction structural frames, walkway handrails, sewage tank purlins and equipment support frames, as their flat sides make installation and connection much easier without additional anti-rotation treatment.
For those special sections produced by custom GFRP pipe pultrusion mold, their application value is even more irreplaceable. Multi-lumen FRP tubes are often used in electrical equipment that needs to run multiple insulating wires inside one profile, while D-shaped and elliptical profiles are very common in tool handles, agricultural equipment components and transportation vehicle lightweight structural parts. This high shape flexibility makes TOLIKE FRP tube pultrusion die a very cost-effective tooling choice for industrial buyers who need to develop diversified composite profile products for different market segments.